
High Purity Sodium Bicarbonate China Factory Suppliers Food and Pharma Grade Baking Soda


Our premium Food-Grade Sodium Bicarbonate is a high-purity white crystalline powder, meticulously engineered for excellence in the food processing, pharmaceutical, and chemical industries. Renowned for its exceptional solubility and stable alkaline properties, this versatile leavening agent is the ideal choice for baking and pastry applications, ensuring consistent aeration, texture, and quality in every batch.
Leveraging a sophisticated carbonization synthesis and multi-stage recrystallization purification process, we deliver a product that strictly adheres to national safety standards. Whether used for pH regulation, buffering, or decontamination, our sodium bicarbonate provides a reliable, low-cost solution for professional manufacturers seeking purity, stability, and direct-from-factory efficiency.
| Product Name | Sodium Bicarbonate (Baking Soda) | Food Grade Purity | ≥99.0% |
|---|---|---|---|
| Industrial Grade Purity | ≥98.5% | Pharmaceutical Grade Purity | ≥99.5% |
| Appearance | White Crystalline Powder | Odor/Taste | Odorless, Salty Taste |
| pH Value (Aqueous) | Approximately 8.3 (Weakly Alkaline) | Solubility | Highly Soluble in Water |
| Production Process | Carbonization Synthesis + Recrystallization | Compliance | National Food & Pharma Standards |
Food-grade purity of ≥99%, ensuring heavy metals and chlorides are well below national safety limits.
Provides mild alkalinity for precise pH buffering without corroding sensitive equipment.
Three rounds of inspection: raw materials, central control, and third-party finished product testing.
Efficiently serves as a leavening agent, acid-base regulator, and cleaning catalyst.
Consistent white color with no visible impurities, meeting the strictest visual food standards.
Manufactured under a strict closed-loop system to prevent contamination throughout production.
Direct factory supply ensuring stable inventory and reduced procurement costs for bulk buyers.
Advanced carbonization synthesis technology for superior chemical consistency.
Real-time central control monitoring for immediate deviation detection during synthesis.
Rigorous tracking of food and pharmaceutical grade standards across all batches.
Optimized packaging and delivery systems to maintain product purity during transit.
Multi-stage recrystallization logic to ensure impurity levels remain far below limits.
| Grade Option | Purity Level | Primary Application |
|---|---|---|
| Food Grade | ≥99.0% | Baking, Pastry, Food Processing |
| Industrial Grade | ≥98.5% | Water Treatment, Desulfurization |
| Pharmaceutical Grade | ≥99.5% | Medical Excipients, Pharma Grade |
| Standard Market Grade | Variable | General Cleaning, Basic Industrial |
| Direct Factory Grade | Optimized | Bulk Manufacturing & OEM |
Food-grade has a purity of ≥99.0% with strict limits on heavy metals and impurities for human consumption, while industrial-grade (≥98.5%) is optimized for technical applications like water treatment.
When heated or reacted with acid, sodium bicarbonate decomposes to release carbon dioxide gas, which creates bubbles and causes the dough or batter to rise.
Yes, our pharmaceutical-grade sodium bicarbonate complies with pharmacopoeia standards with a purity of ≥99.5% and rigorous impurity control.
Each batch undergoes three rounds of QC: initial raw material inspection, random central control sampling, and final third-party re-inspection.
Absolutely. Our sodium bicarbonate is widely used in water treatment for pH regulation, buffering, and stabilization due to its mild alkalinity.
No, our high-purity sodium bicarbonate is odorless and completely free of visible impurities to the naked eye, meeting strict food safety requirements.

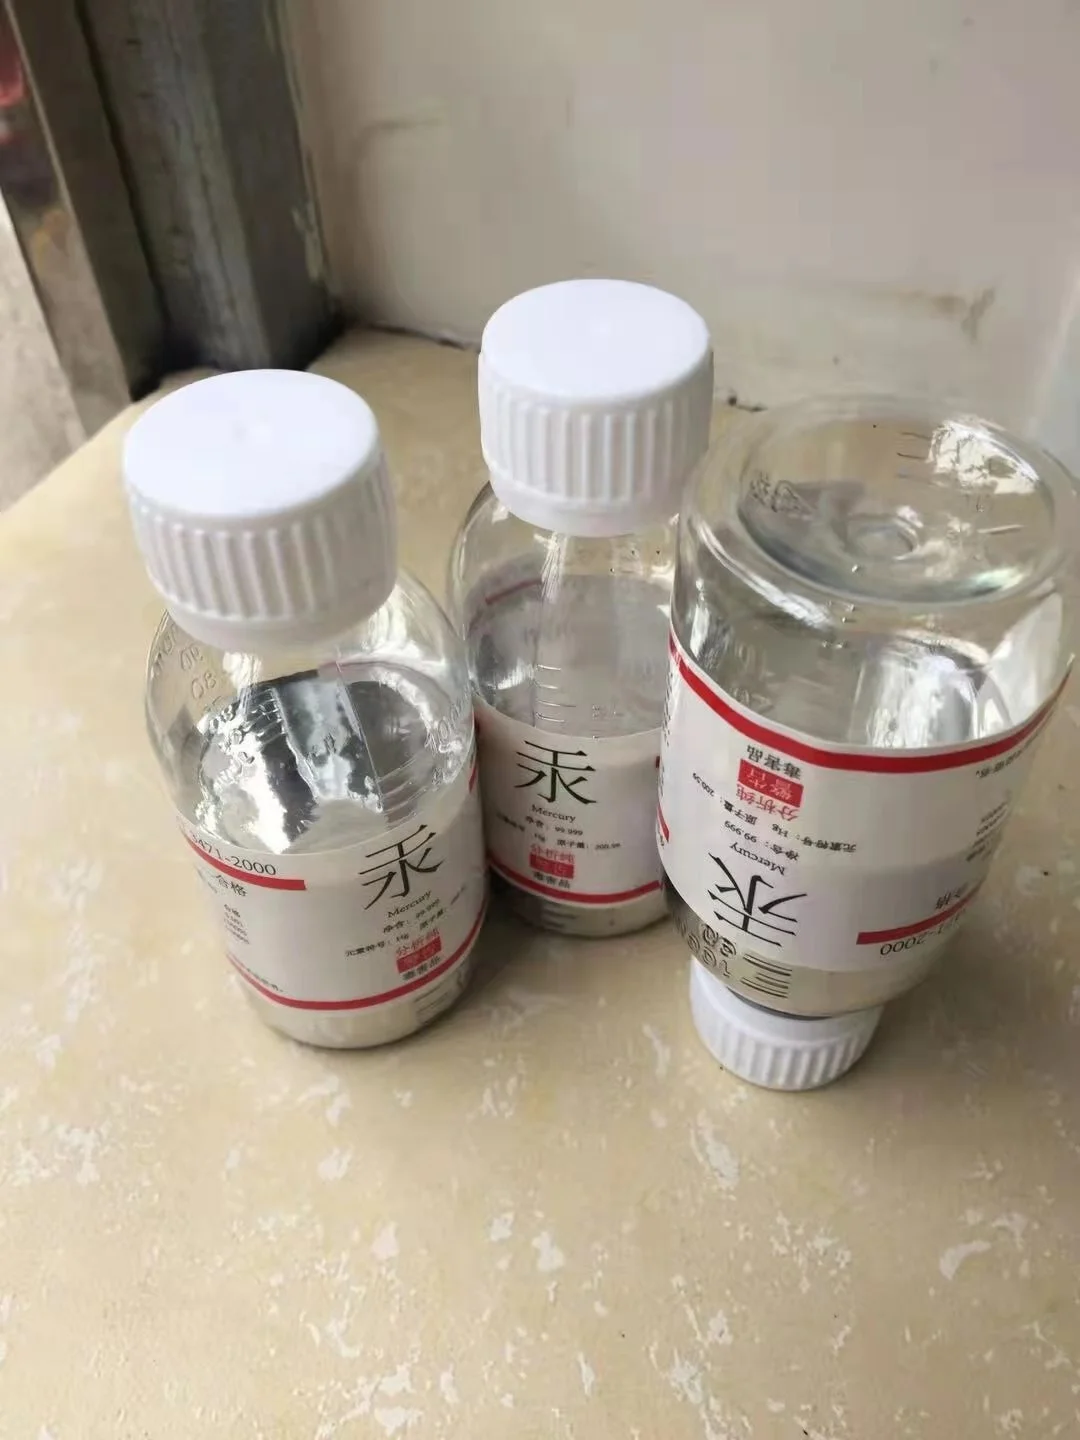
Looking for premium Liquid Mercury Hg? As leading China suppliers and a certified factory, we provide 99.999 purity mercury for gold extraction, thermometers, and sphygmomanometers with full export compliance.
Product Description
Mercury, chemically known as mercury (Hg), is the only metal that exists in liquid form at normal temperature and pressure. It has a silvery-white metallic luster, is highly fluid and has an extremely high density (13.59 g/cm³). Its unique physical and chemical properties, such as a low melting point (-38.87℃), high boiling point (356.6℃), stable coefficient of thermal expansion, and extremely low vapor pressure, make it a core material for many special products.
Basic Info
Product Name | Mercury |
Content (Hg)% | ≥99.999% |
Iron (Fe)% Iron (FE)% | ≤0.00002 |
Other heavy metals (in lead)% | ≤0.00004 |


Looking for premium Liquid Mercury Hg? As leading China suppliers and a certified factory, we provide 99.999 purity mercury for gold extraction, thermometers, and sphygmomanometers with full export compliance.
Product Description
Mercury, chemically known as mercury (Hg), is the only metal that exists in liquid form at normal temperature and pressure. It has a silvery-white metallic luster, is highly fluid and has an extremely high density (13.59 g/cm³). Its unique physical and chemical properties, such as a low melting point (-38.87℃), high boiling point (356.6℃), stable coefficient of thermal expansion, and extremely low vapor pressure, make it a core material for many special products.
Basic Info
Product Name | Mercury |
Content (Hg)% | ≥99.999% |
Iron (Fe)% Iron (FE)% | ≤0.00002 |
Other heavy metals (in lead)% | ≤0.00004 |


Sodium cyanide is a white crystalline powder at normal temperature and pressure. It is highly soluble in water, and its aqueous solution is strongly alkaline.
Sodium cyanide is an important chemical raw material, mainly applied in the following fields:
Electroplating industry: It is used for electroplating and surface treatment of metals, which can enhance the smoothness and adhesion of the coating.
Metallurgical industry: It is used for extracting precious metals such as gold and silver. By taking advantage of the property that cyanide ions form stable complexes with precious metal ions, it achieves the enrichment and separation of precious metals.
Organic synthesis: As an intermediate, it is used in the manufacture of drugs, dyes, pesticides and other chemicals.
It is widely used for Gold, Silver extraction. It is a main part of plating liquids for zinc,copper, gold, silver, cadmium etc. It also used as the raw material for fine chemicals, pharmaceutical intermediates, pesticide intermediates, etc.
1、In 50kgs iron drums lined with PE bags. Normally in black & blue color, also can be painted according with customer’s request.
2、In 1000kgs wooden boxes,with inner woven bags & PE bags.
| Molecular formula | NaCN | Molar mass | 49.01 g/mol |
| Appearance | white crystalline pills | CAS number | [143-33-9] |
Item | Specification |
Purity (NaCN) | 98.0% min. |
Sodium Hydroxide (NaOH) | 0.5% max. |
Sodium Carbonate (Na2CO3) | 0.5% max. |
Water (H2O) | 0.5% max. |
Water Insoluble | 0.05% max. |