
Premium Xanthan Gum Factory in China High Purity Thickening Agents Suppliers


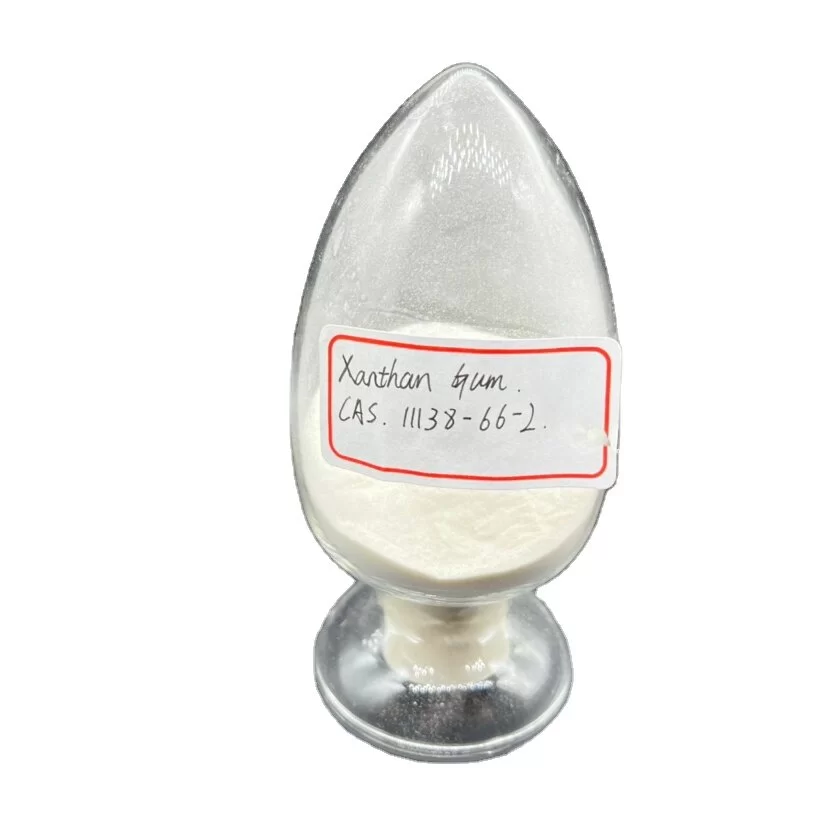
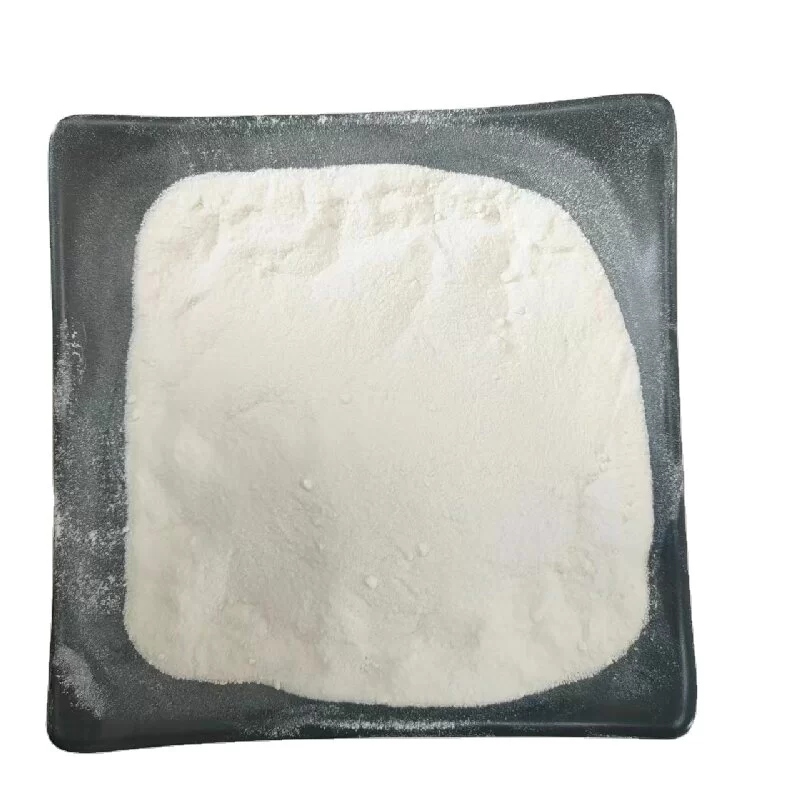
Xanthan Gum is a premium water-soluble high-molecular polysaccharide compound engineered through the advanced fermentation, extraction, and refinement of Xanthomonas campestris. Appearing as a fine, odorless, and tasteless white to light yellow powder, it serves as a versatile multi-functional additive. Its exceptional ability to provide thickening, suspending, emulsifying, and stabilizing effects makes it an indispensable component across diverse industrial applications.
Engineered for resilience, our Xanthan Gum exhibits outstanding stability against acids, alkalis, salts, and high-temperature environments. Whether utilized in high-end food processing, complex water treatment systems, oilfield exploitation, or daily chemical formulations, it ensures a uniform system and prevents stratification, delivering superior performance that significantly optimizes production efficiency and end-product quality.
| Chemical Name | Xanthan Gum | Appearance | White to Light Yellow Powder |
|---|---|---|---|
| Purity Level | ≥ 99% | Odor/Taste | Odorless and Tasteless |
| Food Grade Standard | GB 1886.1-2016 | Industrial Viscosity | ≥ 1200 mPa · s |
| Solubility | Water-soluble | Function | Thickening & Stabilizing |
| Thermal Stability | High Temperature Resistant | Chemical Resistance | Acid, Alkali, and Salt Resistant |
Maintains structural integrity and viscosity under harsh conditions, including high salinity and extreme pH levels.
Forms high-viscosity pseudoplastic solutions even at extremely low concentrations, reducing additive usage.
Effectively suspends solid particles and oil droplets to prevent sedimentation and ensure long-term uniformity.
Produced via precise biological fermentation and multi-stage purification for a purity level of ≥99%.
Dissolves into a uniform and transparent system, ensuring the visual appeal of beverages and sauces.
Versatile adaptability for food, water treatment, oilfields, and daily chemical industries.
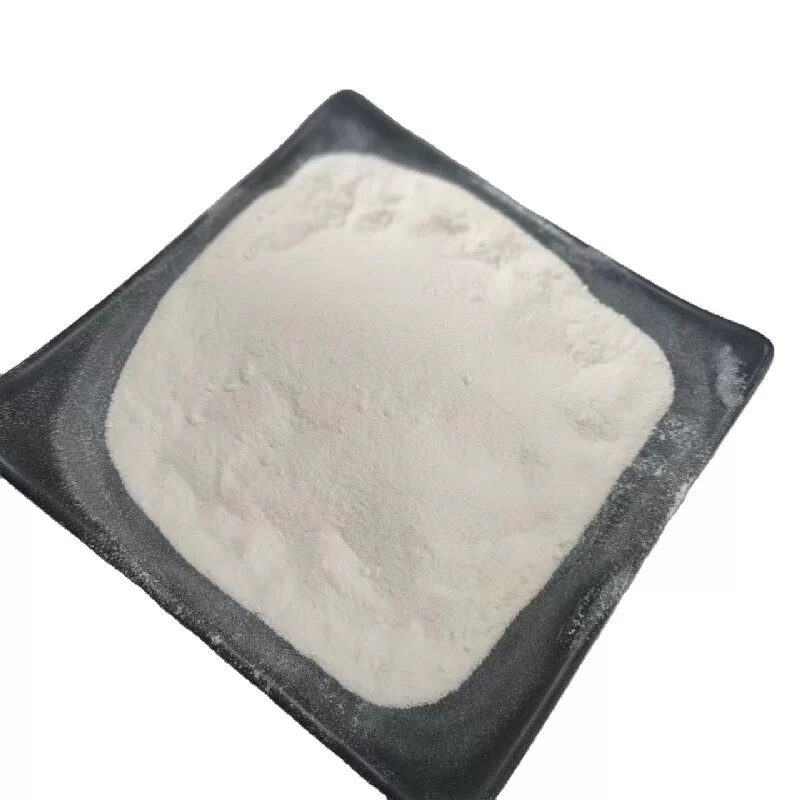
Advanced control of Xanthomonas campestris strains for maximum polysaccharide yield.
Precise fermentation parameter monitoring to ensure consistent batch viscosity.
Rigorous purification processes to eliminate impurities and odors completely.
Strict adherence to GB 1886.1-2016 food-grade standards for safety and purity.
Detailed rheological analysis ensuring stability ≥1200 mPa · s for industrial grades.
Integrated production and logistics for reliable, high-volume chemical supply.
| Feature | Standard Xanthan Gum | Our Premium Xanthan Gum |
|---|---|---|
| Purity Rate | 90% - 95% | ≥ 99% Ultra-Pure |
| Viscosity Stability | Variable by Batch | High Consistency (≥1200 mPa·s) |
| Dosage Requirement | Standard Dosage | Lower Dosage for Equal Effect |
| System Transparency | Slightly Cloudy | Crystal Clear/Transparent |
| Cost Efficiency | Moderate | High (Reduced Waste/Lower Dosage) |
In food production, it acts as a high-efficiency thickening and stabilizing agent, preventing ingredient separation in sauces and beverages while improving mouthfeel and texture.
Yes, our Xanthan Gum is specifically engineered for outstanding resistance to salts, acids, and alkalis, making it ideal for brine-based systems and industrial water treatment.
Pseudoplasticity means the viscosity decreases under shear stress (like pumping or pouring) and recovers quickly, facilitating easier transport while maintaining high stability at rest.
Food-grade complies with strict safety standards like GB 1886.1-2016, while industrial-grade focuses on high viscosity stability and cost-performance for oilfields and chemicals.
Absolutely. Its ability to suspend particles and resist chemical degradation makes it an excellent additive for specialized water treatment and mineral processing reagents.
We utilize a combination of high-quality wild rapeseed strains, precise biological fermentation parameters, and a rigorous multi-stage purification process to achieve ≥99% purity.

Looking for premium Liquid Mercury Hg? As leading China suppliers and a certified factory, we provide 99.999 purity mercury for gold extraction, thermometers, and sphygmomanometers with full export compliance.
Product Description
Mercury, chemically known as mercury (Hg), is the only metal that exists in liquid form at normal temperature and pressure. It has a silvery-white metallic luster, is highly fluid and has an extremely high density (13.59 g/cm³). Its unique physical and chemical properties, such as a low melting point (-38.87℃), high boiling point (356.6℃), stable coefficient of thermal expansion, and extremely low vapor pressure, make it a core material for many special products.
Basic Info
Product Name | Mercury |
Content (Hg)% | ≥99.999% |
Iron (Fe)% Iron (FE)% | ≤0.00002 |
Other heavy metals (in lead)% | ≤0.00004 |

Product Details
| Customization: | Available |
|---|---|
| CAS No.: | 7699-45-8 |
| Formula: | Znbr2 |

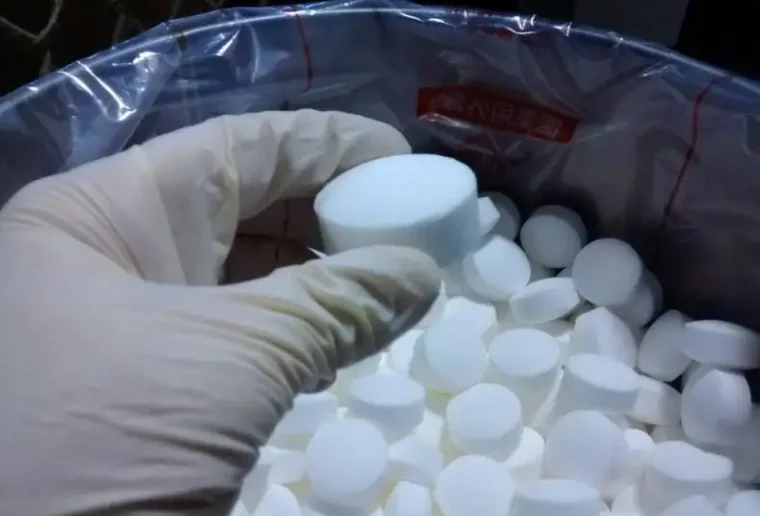
Sodium cyanide is a white crystalline powder at normal temperature and pressure. It is highly soluble in water, and its aqueous solution is strongly alkaline.
Sodium cyanide is an important chemical raw material, mainly applied in the following fields:
Electroplating industry: It is used for electroplating and surface treatment of metals, which can enhance the smoothness and adhesion of the coating.
Metallurgical industry: It is used for extracting precious metals such as gold and silver. By taking advantage of the property that cyanide ions form stable complexes with precious metal ions, it achieves the enrichment and separation of precious metals.
Organic synthesis: As an intermediate, it is used in the manufacture of drugs, dyes, pesticides and other chemicals.
It is widely used for Gold, Silver extraction. It is a main part of plating liquids for zinc,copper, gold, silver, cadmium etc. It also used as the raw material for fine chemicals, pharmaceutical intermediates, pesticide intermediates, etc.
1、In 50kgs iron drums lined with PE bags. Normally in black & blue color, also can be painted according with customer’s request.
2、In 1000kgs wooden boxes,with inner woven bags & PE bags.
| Molecular formula | NaCN | Molar mass | 49.01 g/mol |
| Appearance | white crystalline pills | CAS number | [143-33-9] |
Item | Specification |
Purity (NaCN) | 98.0% min. |
Sodium Hydroxide (NaOH) | 0.5% max. |
Sodium Carbonate (Na2CO3) | 0.5% max. |
Water (H2O) | 0.5% max. |
Water Insoluble | 0.05% max. |